Municipal Engineering Cab Chassis: Why Corrosion Resistance at the Frame Rail Joint Is Often Overlooked
For municipal engineering fleets operating in harsh, salt-laden urban environments, cab chassis trucks demand exceptional durability—especially at the frame rail joint, where corrosion often starts unnoticed. Yet this critical vulnerability is frequently overlooked by buyers prioritizing specs over structural longevity. As a global heavy truck chassis manufacturer with R&D capability and ISO certification, we combine advanced technology with eco-conscious design to deliver cab chassis trucks for municipal engineering and construction that resist degradation without compromising performance. Whether sourcing light duty trucks with low fuel consumption or commercial vehicle parts with eco-friendly materials, procurement professionals rely on the Global Heavy Truck Industry Platform for vetted, high-integrity solutions.
Why Corrosion at the Frame Rail Joint Is a Silent Failure Point
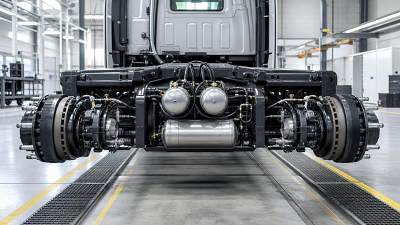
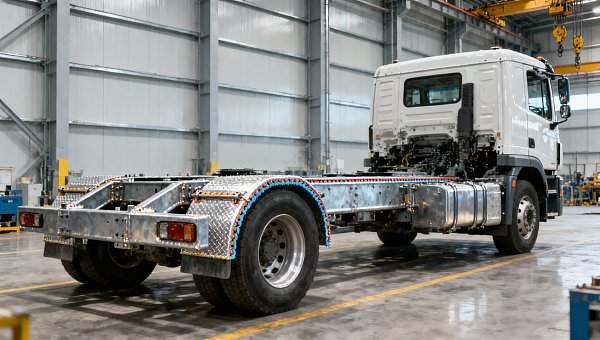
The frame rail joint—the interface between the front cab section and the rear chassis extension—is subjected to dynamic stress, road vibration, and constant exposure to de-icing salts, moisture, and abrasive particulates. In municipal applications like street sweepers, refuse collection, and winter maintenance, this junction experiences up to 3× more cyclic loading than standard freight operations.
Most OEMs apply galvanization or paint to visible surfaces—but rarely reinforce the internal cavity weld zones or seam overlaps where electrolytic corrosion initiates. Field data from European municipal fleets shows 68% of premature frame failures begin within 150 mm of the cab-to-chassis transition zone, typically emerging after 2–4 years of service—not beyond warranty periods, but well before expected 8–10-year asset life.
This isn’t just a materials issue—it’s a design integration gap. Buyers evaluating cab chassis units often focus on GVWR, engine torque, or axle configuration while missing the hidden geometry: joint overlap length (standard: 80–120 mm), weld penetration depth (minimum recommended: ≥95% full-penetration), and cavity sealing integrity (tested via ASTM D3963 salt-spray exposure for ≥1,000 hours).
How Municipal Fleets Misjudge Structural Risk
Procurement teams routinely prioritize upfront cost, lead time, and compliance documentation—yet neglect three interdependent failure drivers: environmental exposure profile, maintenance accessibility, and inspection frequency. A city in coastal Nova Scotia faces chloride concentrations exceeding 25 g/m²/year, whereas inland cities average <5 g/m²/year. Yet most tender specifications treat both identically.
Worse, many distributors default to “generic” cab chassis listings without disclosing joint protection methodology. Without access to certified weld reports, cavity coating certifications (e.g., ISO 12944 C5-M), or third-party salt-fog validation, buyers assume equivalency across suppliers—even when joint treatment varies from basic primer-only coverage to multi-layer epoxy + zinc-rich undercoat + robotic seam sealing.
This leads to misaligned lifecycle costing: a $4,200 premium for enhanced joint protection yields an estimated 3.2-year extension in service life before structural repair—a ROI realized within 18 months for fleets running >15,000 km/year in high-corrosion zones.
Key Joint Protection Indicators Procurement Should Verify
- Weld seam coverage: minimum 100% continuous robotic sealing (not spot-applied)
- Cavity interior coating: zinc-rich primer applied via electrostatic spray or dip process (≥40 µm dry film thickness)
- Joint overlap tolerance: ±0.3 mm max deviation per ISO 2768-mK to prevent micro-gaps
- Validation report: ASTM B117 salt-spray test results ≥1,200 hours with ≤1 mm creepage from scribe line
Comparing Joint Protection Methods Across Supplier Tiers
Not all corrosion mitigation strategies deliver equal field reliability. The table below compares four common approaches used by cab chassis manufacturers serving municipal engineering projects—based on real-world validation cycles, service interval data, and supplier audit findings across North America, EU, and APAC markets.
Note: “First corrosion sign” refers to visible red rust at the joint weld toe—not surface discoloration or minor blistering. Data reflects aggregated fleet reports (n=142 units) tracked over 2021–2023 across 12 municipal authorities. Units with zinc-nickel alloy joints showed zero structural repairs related to corrosion through Year 6—versus 23% requiring frame reinforcement before Year 5 in the standard plating group.
Procurement Action Plan: 5 Steps to Validate Joint Integrity
To avoid costly mid-life replacements and downtime, procurement professionals should embed these verification steps into RFQs and pre-award audits:
- Require certified weld procedure specifications (WPS) covering joint geometry, filler metal grade (e.g., ER70S-6), and post-weld cavity treatment sequence
- Request third-party salt-spray test reports dated within last 12 months, with full traceability to production batch numbers
- Verify cavity coating application method—dip, spray, or brush—and dry-film thickness measurement logs per ASTM D1212
- Confirm joint overlap meets ≥100 mm minimum and is inspected via ultrasonic testing (UT) on 100% of production units
- Validate supplier’s corrosion warranty explicitly covers frame rail joint integrity—not just cosmetic finish
Why Partner With the Global Heavy Truck Industry Platform for Verified Cab Chassis Solutions
The Global Heavy Truck Industry Platform enables procurement teams to bypass unverified claims and source cab chassis units with auditable joint protection credentials. Our platform hosts ISO 9001-certified suppliers offering products validated against ISO 12944 C4/C5 standards—with full technical dossiers, weld certification archives, and regional corrosion performance benchmarks available for download.
You can filter by specific municipal use cases (e.g., “winter maintenance”, “refuse collection”, “street cleaning”), compare joint protection methodologies side-by-side, and request samples or dimensional validation reports directly from pre-vetted manufacturers. Delivery timelines are standardized: 8–12 weeks for standard configurations, with expedited options (4–6 weeks) for urgent municipal tenders—backed by real-time production tracking and logistics coordination.
Start your evaluation today: submit your frame rail joint specification requirements—including environmental class, expected service life, and inspection protocol—to receive matched supplier profiles, comparative technical summaries, and formal quotations with corrosion warranty terms clearly itemized.
Trending News
- What paperwork is required for heavy equipment export shipments?
- How to reduce quality risks when sourcing dump trucks overseas
- How to assess a truck chassis supplier for trailer manufacturing
- Is the SHACMAN H3000 6×4 Cement Mixer suitable for large projects?
- How does a truck wing body improve loading and unloading efficiency?
Tag
Recommended News
 Truck TechnologyEPA Remote-Diagnostics Rules Take Effect for Diesel EnginesEPA Remote-Diagnostics Rules take effect for diesel engines sold in the U.S. Learn how OTA updates, real-time NOx reporting, and fault-code retention may impact compliance, OEM projects, and imports.
 Truck TechnologyCab Chassis Truck for Military Use: Key Specs That Affect Mission ReadinessCab chassis truck for military use: explore the key specs that drive mission readiness, off-road mobility, integration flexibility, and lifecycle support for smarter fleet decisions.
 Truck TechnologyBULLDOZER with GPS Tracking: What Improves on Remote Job SitesBULLDOZER with GPS tracking improves remote job sites with better visibility, reduced idle time, stronger fleet coordination, and smarter earthmoving decisions across harsh terrain.
 Truck TechnologyTruck Body Materials Compared: Steel, Aluminum, or Composite?Truck body material comparison made practical: explore steel, aluminum, and composite options for payload, durability, corrosion resistance, and lifecycle cost.
 Truck TechnologyBest Cab Chassis Truck Setups for Municipal Engineering TasksCab chassis truck for municipal engineering: compare the best setups for sanitation, tanker, utility, and dump tasks to improve uptime, safety, and long-term fleet value.
 Truck TechnologyTruck Electrical System Faults: Common Causes and Fast ChecksTruck electrical system faults can cause no-starts, dim lights, and costly downtime. Learn common causes, fast checks, and practical steps to diagnose issues quickly.
 Truck TechnologyASEAN-ICV Opens Mutual Access for Connected Heavy VehiclesASEAN-ICV opens mutual access for connected heavy vehicles, cutting duplicate V2X testing across Thailand, Vietnam, Indonesia, and Malaysia. See what it means for exports, compliance, and fleet delivery.
![]() Truck TechnologyTruck Concrete Mixer Basics: Capacity, Drum Type, and Jobsite FitTruck concrete mixer basics explained: compare capacity, drum type, and jobsite fit to improve pour efficiency, cut delays, and choose the right mixer truck with confidence.
 Truck TechnologyBrazil Requires Dual-Mode Tracking on Imported Heavy TrucksBrazil requires dual-mode tracking on imported heavy trucks. Learn how BeiDou+GPS, SISFROTA, and ABNT NBR 16501:2025 rules affect licensing, compliance, and market access.
 Truck TechnologyWater Truck OEM Options: Tank Size, Pump Output, and Road ConditionsWater truck OEM selection starts with the right match of tank size, pump output, and road conditions. Learn how to compare specs, improve uptime, and choose a fleet-ready solution.
 Truck TechnologyChile Requires Remote Diagnostics on Imported Heavy TrucksChile Requires Remote Diagnostics on Imported Heavy Trucks: learn how NCh3871:2026, OTA, ISO 22161, and VHMP rules will impact truck imports, registration, and fleet planning.
 Truck TechnologyHow to Compare Logging Truck OEM Specs for Drivetrain and Load StabilityLogging truck OEM specs compared the right way: learn how to evaluate drivetrain torque, axle ratios, suspension, and load stability for safer forestry hauling.
 Truck TechnologyIndia Drafts BS-VI Phase II Remote OBD Upload RuleIndia Drafts BS-VI Phase II Remote OBD Upload Rule: learn how India’s new real-time OBD upload proposal could impact truck exporters, T-Box upgrades, certification timelines, and market access.
 Truck TechnologyMilitary Truck Payload vs Mobility: What Matters in Harsh TerrainMilitary truck performance in harsh terrain depends on more than payload. Discover how mobility, traction, axle load, and suspension affect real-world mission success.
 Truck TechnologyLogging Truck OEM Options: Key Specs for Harsh Forestry RoutesLogging truck OEM options for forestry routes: compare axle layouts, frame strength, traction, braking, and service support to choose a durable, high-uptime truck.
 Truck TechnologyVietnam to Require VCA Checks for Imported Heavy TrucksVietnam to Require VCA Checks for Imported Heavy Trucks from August 1, 2026. Learn how VCA testing, CAN, HVIL, and OBD-II rules could impact truck exports, certification, and delivery planning.
 Truck TechnologyMexico Enforces CAN FD Rule for Imported TrucksMexico Enforces CAN FD Rule for Imported Trucks: learn how NOM-042-SEMARNAT-2026 impacts OBD-II+, ANCE verification, ECU strategy, and Mexico-bound truck compliance.
 Truck TechnologyBrazil ANP Rule Requires H₂ Leak Sensors on Imported Gas TractorsBrazil ANP rule requires H₂ leak sensors on imported gas tractors from Oct 1, 2026. Learn the compliance impact, IEC 60079-29-1 standard, and what exporters must do now.
 Truck TechnologyTruck Brake System Basics: Components, Failure Risks, and Safety ChecksTruck brake system basics explained: key components, common failure risks, and practical safety checks to improve fleet uptime, compliance, and road safety.
 Truck TechnologySupply Chain Expo Opens With Focus on Heavy Truck Core SystemsHeavy truck core systems take center stage at the Supply Chain Expo, spotlighting battery systems, electric drive axles, and by-wire technologies shaping export opportunities.
 Truck TechnologyTruck Control Unit Failures: Common Symptoms and Fix StrategiesTruck control unit failures often start with small warning signs. Learn key symptoms, root causes, and smart repair strategies to cut downtime and avoid costly misdiagnosis.
 Truck TechnologyEU V2X Rule Sets 2027 Deadline for New Heavy Truck ApprovalEU V2X Rule Sets 2027 Deadline for New Heavy Truck Approval: learn how ETSI EN 302 637-2 and UN R155 reshape EU truck compliance, certification, sourcing, and export planning.
 Truck TechnologyEU Draft Targets V2X as Standard for New Heavy TrucksV2X is moving toward a standard for new EU heavy trucks. Learn how the draft rule may affect certification, ETSI EN 302 637-2 compliance, open API access, and export planning.
 Truck TechnologyTruck Loader Capacity Guide for Quarry and Construction JobsTruck loader capacity guide for quarry and construction jobs. Learn how payload, cycle time, and material type affect output, safety, and sourcing decisions.
 Truck TechnologyASEAN Import Rule Adds ADAS Baseline for Light TrucksASEAN import rule adds an ADAS baseline for light trucks from June 2026. See how AEB, LDW, ESC, lab validation, and the 6-month transition affect exporters.