How to evaluate quality control before choosing a truck trailer OEM
Choosing a truck trailer OEM is often treated as a comparison of payload, dimensions, axle configuration, and quoted price. Those factors matter, but they do not reveal whether the trailer will remain safe, compliant, and economically serviceable after thousands of kilometres on uneven roads, under variable loads, and through repeated loading cycles.
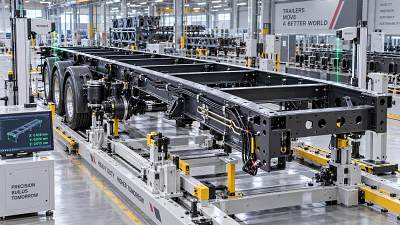
For a procurement decision, quality control should be assessed as a production system rather than a final inspection activity. A trailer that looks acceptable at dispatch may still develop early fatigue cracking, brake imbalance, corrosion around joints, deck deformation, or electrical failures if the OEM has weak control over design validation, incoming materials, welding, assembly, and change management.
The practical question is not whether a manufacturer says it has quality control. Nearly every supplier will say that it does. The question is whether its processes can consistently produce trailers matching the agreed specification, applicable regulations, and operating conditions of the buyer’s fleet.
Start with the operating profile, not the factory brochure
Quality requirements are inseparable from the intended application. A standard curtain-side semi-trailer operating mainly on paved intercity routes faces a different risk profile from a tipper trailer serving a quarry, a skeletal trailer carrying containers to port terminals, or a low-bed trailer used for construction equipment.
Before evaluating a truck trailer OEM, procurement teams should define the duty cycle in terms that can be translated into engineering and inspection requirements:
- Gross combination weight, payload range, and expected load concentration;
- Road conditions, gradients, off-road exposure, and frequency of uneven terrain;
- Annual mileage and expected service life;
- Loading method, including forklifts, cranes, ramps, tippers, or container handlers;
- Climate exposure, especially coastal salt, high humidity, extreme heat, cold, or abrasive dust;
- Tractor compatibility, fifth-wheel height, electrical connections, braking interfaces, and axle-load requirements;
- Destination-market approval, registration, and safety requirements.
Without this baseline, quality discussions tend to become vague. For example, a buyer may ask for a “reinforced chassis” without defining where the reinforcement is needed or what loading event it must withstand. This can lead to excess steel in low-stress areas while critical interfaces—kingpin zone, suspension brackets, cross-member joints, landing gear supports, or rear bumper structure—remain insufficiently engineered.
A competent OEM should ask detailed application questions before finalising the design. A supplier that accepts a generic specification immediately may be efficient in sales, but that is not evidence of engineering discipline.
Examine whether design control exists before inspecting production quality
Manufacturing quality cannot compensate for an inadequately validated design. The most consequential trailer failures often originate in design assumptions: underestimated fatigue loads, poor stress distribution around welded joints, unsuitable material grades, incompatible component selection, or insufficient protection against corrosion and water ingress.
Buyers do not need to independently verify every engineering calculation, but they should establish whether the manufacturer uses a repeatable design-control process. Useful questions include whether the OEM maintains controlled drawings and bills of materials, conducts formal design reviews, applies finite element analysis where appropriate, and validates new or modified designs through prototype testing or documented field feedback.
Particular attention should be given to designs that are new to the OEM or materially different from its established production models. A manufacturer may have strong experience with flatbeds but limited practical data on aluminium tankers, extendable trailers, heavy-haul low loaders, or mine-service tipping bodies. In such cases, previous deliveries of a visually similar product are not enough. Procurement should request evidence that the critical design features have been assessed for the intended load case.
Design change control is equally important. If an axle, landing gear, steel grade, brake valve, or suspension bracket is substituted after approval, the change can affect compliance, durability, spare-parts compatibility, and axle-load distribution. The purchase contract should require written approval for substitutions affecting safety-critical, regulatory, or performance-related components.
Material traceability is a meaningful indicator of manufacturing discipline
The steel in a trailer frame is not a commodity detail. Structural strength, weldability, fatigue performance, and corrosion resistance all depend on the correct material being used in the correct location. The same principle applies to axle beams, kingpins, suspension components, fasteners, brake parts, hydraulic cylinders, and electrical harnesses.
A credible truck trailer OEM should be able to show how it controls incoming materials. This generally includes supplier qualification, purchase specifications, receiving inspection, storage segregation, and records linking critical materials to production batches. For structural steel, mill test certificates can help confirm grade and chemical or mechanical properties, but the value lies in traceability rather than paperwork alone. A certificate that cannot be connected to the actual plate or section used in a trailer provides limited assurance.
During a factory audit, buyers should observe whether material identification is retained after cutting and whether different grades or thicknesses are clearly separated. Misidentification can be difficult to detect once a trailer is painted. It is particularly relevant when high-strength steels are used, since unapproved substitutions may change forming behaviour and welding requirements.
Component sourcing deserves the same scrutiny. Braking systems, axles, suspensions, couplings, landing legs, tyres, lighting, and electrical connectors have direct effects on safety and operating availability. Procurement should ask for approved component lists that identify manufacturer, model, technical rating, and country of origin. Terms such as “equivalent brand” should not be accepted for components specified by name, approval, or performance rating.
Welding quality should be assessed as a controlled process, not judged by appearance
Trailer structures rely heavily on welded assemblies. A smooth-looking weld bead is not proof of a sound joint, while a visually imperfect but acceptable weld may not indicate a structural defect. The important issue is whether the OEM controls welding procedures, personnel competence, fit-up, consumables, heat input, inspection, and repair.
For steel structures, an established manufacturer should be able to provide welding procedure documentation appropriate to the materials and joint types being used. Depending on the market and project requirements, buyers may also encounter frameworks such as ISO 3834 for quality requirements in fusion welding, ISO 14731 for welding coordination, and qualifications based on relevant welding standards. These documents should be interpreted in context: certification can support confidence in a process, but it does not replace inspection of the actual factory operation.
A site visit often reveals more than a certificate. Look for clean weld preparation, stable fixtures, controlled part alignment, dry storage of consumables where required, and clear separation between completed and uninspected assemblies. Check whether welders work from approved drawings and procedures rather than relying solely on personal experience.
Ask how the OEM inspects high-stress locations, including the kingpin plate and neck area, main beam connections, suspension hangers, tipping pivot assemblies, drawbar connections, and landing gear mounting points. Visual inspection is fundamental, but certain critical welds may warrant non-destructive testing such as magnetic particle, ultrasonic, or dye penetrant examination, depending on the design, customer specification, and applicable regulations.
The buyer should also ask how weld repairs are recorded and approved. Rework is not automatically a sign of poor quality; unmanaged rework is. Repeated repair in the same structural area can create distortion or affect fatigue performance if it is not controlled.
Verify dimensional control and assembly accuracy
Trailer quality is also determined by geometry. Misalignment of axles, suspension mounts, kingpins, doors, decks, or twist locks can create tyre wear, unstable handling, water ingress, difficult coupling, cargo damage, and accelerated component failure.
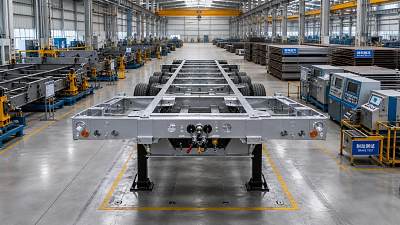
The OEM should have defined inspection points for chassis squareness, axle alignment, kingpin location, ride height, wheelbase, suspension geometry, and body dimensions. The specific tolerances depend on the trailer type and market, but the buyer should expect the supplier to work against controlled limits rather than informal judgement.
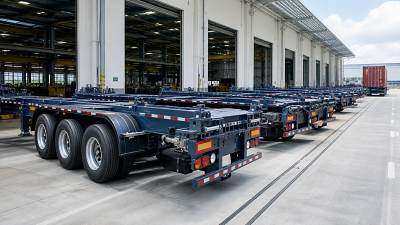
For container skeletal trailers, verify twist-lock position, locking operation, and compatibility with the container sizes ordered. For box and refrigerated bodies, examine door sealing, floor flatness, panel joints, and water-management details. For tippers, assess body alignment, hinge geometry, hydraulic installation, and stability-related features. For low-bed trailers, ramp function, deck transition points, hydraulic synchronization, and tie-down arrangement deserve particular scrutiny.
Axle alignment should not be treated as a minor final-stage check. A poorly aligned multi-axle trailer can consume tyres quickly and generate operating complaints that are costly to diagnose after export. Buyers should request the OEM’s alignment method, inspection records, and corrective procedure when readings fall outside its acceptance criteria.
Look beyond paint: corrosion protection is a lifecycle issue
Paint quality is one of the easiest features to inspect visually and one of the easiest to overestimate. A glossy finish at the factory says little about surface preparation, coating adhesion, edge coverage, cavity protection, or resistance to stone impact and salt exposure.
For export trailers, corrosion control should be matched to the operating environment. Standard painted steel may be adequate for dry inland logistics operations but less suitable for coastal, winter-road, chemical, agricultural, or mining environments. The relevant questions are practical: Was the surface properly prepared? Are sharp edges treated? Are weld spatter and contaminants removed? Are drain paths provided? Are enclosed sections protected or sealed? Can water collect at cross-members, hinges, subframes, and body joints?
If the supplier proposes shot blasting, zinc-rich primer, galvanising, hot-dip galvanised components, or multi-layer coating systems, request the defined process and inspection records. Dry-film thickness measurement, adhesion checks, and visual inspection should be documented where they form part of the agreed quality plan. Galvanising is not automatically the best answer for every design; it may affect distortion, venting requirements, repair methods, and downstream fabrication. The decision should be based on the environment and structure, not on a simple “galvanised equals better” assumption.
Confirm that testing covers the trailer’s actual safety functions
End-of-line testing should demonstrate that the finished unit functions as specified. The exact test scope will vary by trailer type and destination market, but buyers should expect documented checks of braking, lighting, electrical connections, pneumatic systems, hydraulic systems where fitted, coupling interfaces, and basic roadworthiness.
Braking compliance is particularly sensitive. Requirements differ across markets. In jurisdictions applying UNECE regulations, brake-system requirements may involve UNECE Regulation No. 13. In the United States, relevant federal requirements include FMVSS No. 121 for air brake systems on applicable vehicles. Other national markets apply their own approval and inspection regimes. Buyers should verify the requirements of the country where the trailer will be registered and operated, rather than assuming that a general export declaration is sufficient.
Ask whether each unit receives a brake test report, air-leak test, lighting check, and functional test of ABS or electronic braking components when installed. For hydraulic tipping equipment, confirmation of safe raising and lowering, hose routing, leakage control, and mechanical safety provisions should be part of final acceptance. For specialised trailers, factory acceptance testing may need to include load-related functional checks agreed before production begins.
A road test can be useful, but it should not become a substitute for disciplined process inspection. By the time a unit reaches the road-test area, most structural and assembly defects are expensive to correct.
Read certifications carefully and distinguish them from product approval
Certification is useful when buyers understand what it proves. ISO 9001, for example, indicates that an organisation has a quality management system assessed against that standard. It does not by itself confirm that every trailer design is fit for a particular duty cycle or that every product meets a destination country’s vehicle approval requirements.
Likewise, a component approval does not automatically approve the complete trailer. Procurement should separate three questions: whether the factory has a documented quality system, whether supplied components meet applicable requirements, and whether the finished trailer can legally be registered and operated in the target market.
For cross-border purchases, request a document matrix before issuing the purchase order. It should identify required certificates, type-approval documents where applicable, component approvals, test reports, serial-number records, manuals, warranty terms, and customs-related documentation. This reduces the common problem of discovering at arrival that a trailer lacks the evidence needed for registration, insurance, fleet acceptance, or project handover.
Audit the factory’s response to defects, not only its stated defect rate
Suppliers may present low defect figures, but metrics are meaningful only if the definitions, inspection coverage, and corrective actions are clear. A more revealing question is what happens when a nonconformity is found.
Ask for examples of recent corrective actions involving structural defects, supplier component failures, paint issues, brake faults, or field complaints. A reliable OEM should be able to explain how it contained the issue, identified root causes, corrected affected stock, and prevented recurrence. This is especially relevant for first-time export orders, where the buyer may have limited ability to return units for rework.
Also assess whether quality records are traceable by trailer serial number. If a fleet reports a recurring issue six months after delivery, the manufacturer should be able to identify the production batch, installed components, inspection results, and any related units. Without this traceability, warranty discussions quickly become difficult.
Build quality requirements into the commercial agreement
Quality expectations that are not written into the contract are often treated as preferences. The technical specification should therefore form part of the purchase agreement and include approved drawings, bill-of-material requirements, component brands or performance criteria, applicable regulations, inspection stages, acceptance standards, required records, and rules for changes.
For larger orders or customised trailers, independent pre-shipment inspection can be valuable, especially when the buyer cannot maintain a permanent quality presence at the factory. The inspector should work from an agreed inspection and test plan rather than a generic checklist. Critical hold points may include material receipt, chassis fit-up before welding closure, axle and suspension installation, coating completion, brake testing, and final documentation review.
Payment terms can reinforce quality discipline when linked to meaningful milestones. However, buyers should avoid creating an inspection process so late or so broad that problems can only be found after most of the manufacturing cost has been incurred. Early technical review and in-process visibility are usually more effective than aggressive final rejection.
Choose the OEM whose controls match the consequences of failure
The lowest-priced trailer can become the most expensive asset if downtime, tyre wear, rejected registration, corrosion repairs, or repeated warranty claims disrupt fleet operations. At the same time, the most elaborate quality system is not automatically justified for a simple, low-utilisation application. The right level of control depends on operating severity, regulatory exposure, order value, service accessibility, and the cost of failure.
When comparing a truck trailer OEM, procurement teams should give greater weight to evidence than to claims: controlled engineering documents, traceable materials, qualified welding processes, measurable assembly checks, documented testing, clear compliance records, and a credible response to field defects. These factors do not eliminate risk, but they make quality more visible before capital is committed.
A dependable manufacturing partner is not defined by a flawless presentation or a long certificate list. It is defined by whether the factory can demonstrate, unit by unit, how it converts an agreed specification into a safe and repeatable product—and how it responds when the process does not perform as intended.
Trending News
- How to reduce quality risks when sourcing dump trucks overseas
- How to assess a truck chassis supplier for trailer manufacturing
- Is the SHACMAN H3000 6×4 Cement Mixer suitable for large projects?
- How does a truck wing body improve loading and unloading efficiency?
- How to evaluate heavy duty trucks for sale in Russia before buying
Tag
Recommended News
 Buying GuideHow to assess a truck chassis supplier for trailer manufacturingTruck chassis supplier for trailer manufacturing: learn how to assess technical fit, quality control, engineering support, and delivery reliability for smarter sourcing.
 Buying GuideIs the SHACMAN H3000 6×4 Cement Mixer suitable for large projects?SHACMAN H3000 6×4 Cement Mixer: assess payload, cycle time, traction, and service support to see if it can keep large concrete projects moving efficiently.
 Buying GuideHow to evaluate heavy duty trucks for sale in Russia before buyingHeavy duty trucks for sale in Russia: learn how to compare specifications, winter readiness, service support, supplier reliability, and total ownership costs before buying.
 Buying GuideWhat to verify before choosing a logging truck producerChoose a logging truck producer with confidence: verify chassis strength, load security, compliance, service support, and delivery control for demanding forestry routes.
 Buying GuideHow to choose a truck excavator for confined construction sitesTruck excavator selection for confined sites: explore access, reach, stability, attachments, and safety factors to choose a productive, space-efficient solution.
 Buying GuideHow to choose a bulk trailer for high-volume aggregate haulingBulk trailer selection guide for high-volume aggregate hauling—optimize payload, body type, safety, compliance, and total cost for reliable fleet performance.
 Buying GuideHow to compare truck tire rolling resistance for lower fleet fuel costsTruck tire rolling resistance explained: compare test data, tread design, maintenance, and total cost to cut fleet fuel costs with confidence.
 Buying GuideHow to evaluate quality control before choosing a truck trailer OEMTruck trailer OEM quality control: learn how to assess design validation, welding, material traceability, testing, compliance, and factory audits before you buy.
 Buying GuideHow to verify a dump truck supplier can meet your delivery deadlineDump truck supplier with quick delivery: learn how to verify stock, production capacity, quality control, and export logistics to keep your project on schedule.
 Buying GuideHow to size a bulldozer for mining operations by haul road gradeBULLDOZER for mining operations sizing guide: match haul road grade, traction, blade capacity, and stability to improve safety, productivity, and fuel efficiency.
 Buying GuideHow to evaluate a construction machinery manufacturer’s quality controlConstruction machinery manufacturer quality control: learn how to assess materials, welding, hydraulics, testing, and after-sales support before you buy.
 Buying GuideHow to verify an excavator manufacturer with CE certificationExcavator manufacturer with CE certification: learn how to verify documents, model traceability, and factory compliance to avoid sourcing risks and buy with confidence.
 Buying GuideHow to evaluate a crane truck exporter before placing a bulk orderCrane truck exporter evaluation made simple: learn how to verify compliance, production capacity, delivery reliability, and after-sales support before placing a bulk order.
 Buying GuideWhen does a refrigerator truck make more sense than insulated transportRefrigerator truck or insulated transport? Learn when a refrigerator truck delivers better temperature control, lower spoilage risk, and smarter cold chain ROI.
 Buying GuideWhen does a tractor truck make more sense than a rigid truck?Tractor truck or rigid truck? Learn when a tractor truck delivers better flexibility, payload efficiency, and long-haul value for growing freight operations.
 Buying GuideHow to choose the right BULLDOZER for land clearing on rough terrainBULLDOZER for land clearing on rough terrain: learn how to choose the right size, tracks, blade, and support setup to improve safety, productivity, and total project value.
 Buying GuideHow to evaluate a semi trailer distributor before placing a bulk orderSemi trailer distributor selection can make or break a bulk order. Learn how to assess technical support, quality control, documentation, delivery reliability, and after-sales service before you buy.
 Buying GuideHow to compare an excavator manufacturer for construction on uptime supportExcavator manufacturer for construction comparison starts with uptime support. Learn how to assess service response, parts availability, training, and escalation to reduce downtime risk.
 Buying GuideHow to choose the right hydraulic pump for truck-mounted equipmentHydraulic pump selection for truck-mounted equipment: learn how to match flow, pressure, PTO, and duty cycle to improve reliability, efficiency, and uptime.
 Buying GuideHow to choose a cab chassis truck for construction jobscab chassis truck for construction buyers: learn how to match payload, body plan, and site conditions to choose the right truck faster and avoid costly mistakes.
 Buying GuideHow to Choose the Right Truck Battery for Reliable Cold StartsTruck battery selection for reliable cold starts can reduce downtime and boost fleet uptime. Learn how to choose the right battery for winter performance.
 Buying GuideHow to Evaluate a Truck Parts Distributor for Lead Time and OEM TraceabilityTruck parts distributor evaluation starts with real stock visibility, lead time accuracy, and OEM traceability. Learn how to compare suppliers and avoid fitment, batch, and delivery risks.
 Buying GuideHow to Choose a Truck Gasket for Heat, Oil, and Pressure ResistanceTruck gasket selection made simple: learn how to choose the right truck gasket for heat, oil, and pressure resistance, avoid failure risks, and compare materials before sourcing.
 Buying GuideHow to Choose an Excavator for Demolition Based on Reach, Attachment Weight, and Jobsite RiskEXCAVATOR for demolition selection starts with real reach, attachment weight, and jobsite risk. Learn how to choose a safer, more productive machine for demanding demolition work.
 Buying GuideHow to Evaluate a Logging Truck Supplier for Payload, Durability, and SupportLogging truck supplier evaluation starts with payload, durability, and after-sales support. Learn what to compare to reduce downtime, control costs, and choose a truck built for real forestry work.